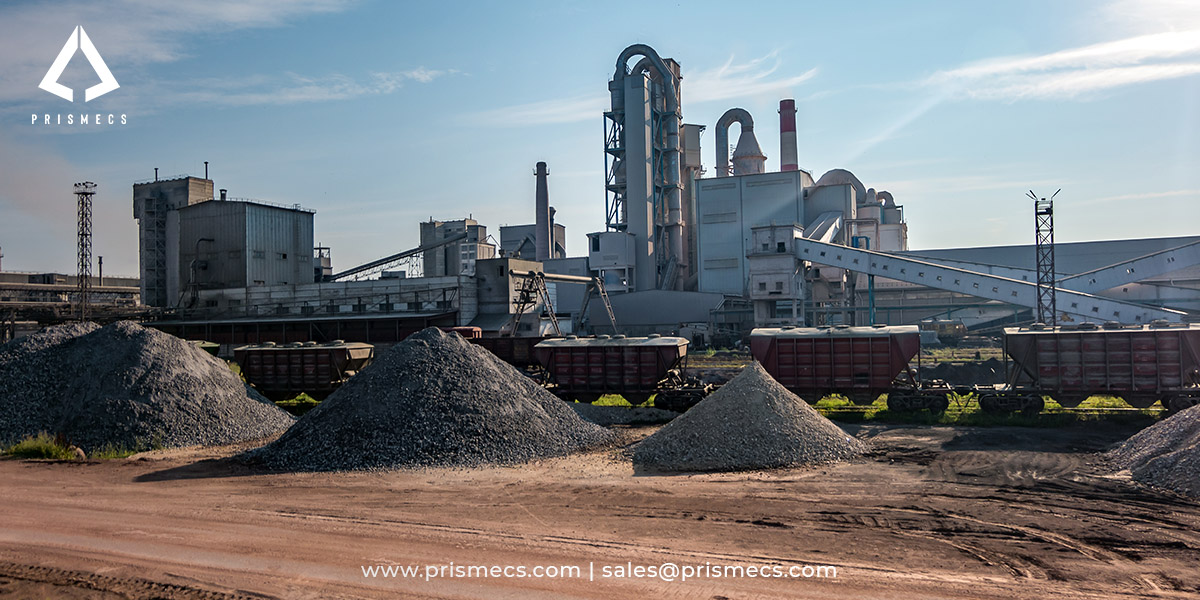
Cement manufacturing runs in seven stages, and the chemistry that matters happens in three of them.
Raw meal is heated to approximately 1450°C in a rotary kiln, where partial melting of 20 to 30 percent allows belite to react with calcium oxide and form alite. That reaction is the source of early strength in the finished cement, and it is reversible. Cool the clinker too slowly and alite converts back to belite between 900°C and 1250°C, destroying what the kiln just produced.
Most process guides stop at the packing line. This one covers the seven stages with the control ratios and temperatures that govern them, the standards that define the product, the energy the plant consumes, and the handful of assets whose failure stops the line.
The Seven Stages
Cement manufacturing runs from quarry to dispatch in seven stages, with the chemistry concentrated in the middle three.
Stages three, four and five are where product quality is determined. Stages one, two, six and seven determine cost.
Quarrying and Crushing
Cement plants are sited at the limestone deposit, because limestone is low-value and heavy and hauling it is the single largest avoidable cost in the process.
The primary raw materials are limestone, which supplies calcium, and clay or shale, which supplies silicon, aluminium and iron. Secondary and corrective materials include marl, chalk, slate, sand, fly ash, mill scale, bauxite and iron ore, added to balance the oxide chemistry.
Cement needs four oxides: calcium oxide, silica, alumina and iron oxide. Everything quarried or imported to the plant exists to deliver those four in the right proportions.
Crushing
Extraction uses controlled blasting or heavy machinery. Primary crushing, typically by jaw or gyratory crusher, reduces the rock to a maximum size of about 6 inches. Secondary crushers or hammer mills then reduce it to about 3 inches or smaller.
The material at this point is ready for raw grinding. For the equipment categories involved, see our overview of mining services equipment.
Why siting matters commercially
A plant at the quarry moves raw material by conveyor. A plant away from it moves raw material by truck, and roughly 1.5 tonnes of raw material are consumed per tonne of clinker. That haulage cost is permanent and it is why almost every integrated cement plant in the world sits on its own deposit.
Raw Meal: Proportioning and the Control Ratios
Raw meal proportioning is where cement quality is set, and it is controlled by three ratios and verified by a fourth calculation.
Limestone makes up approximately 80 percent of the raw mix, and clay or shale the remaining 20 percent, with corrective materials added in small quantities to trim the chemistry. The crushed materials are ground together in a raw mill, blended, and dried so that moisture falls below 1 percent before the meal reaches the preheater.
The four clinker phases
Portland cement clinker consists principally of four compounds, conventionally written in cement chemist notation:
Bogue calculation converts the oxide analysis of the clinker into estimated proportions of these four phases. It is the standard method for relating a chemical analysis to the mineral composition that actually determines performance.
The three control ratios
Lime saturation factor (LSF) expresses how much calcium oxide is present relative to the maximum the silica, alumina and iron can combine with. Too high and free lime results; too low and alite formation is incomplete.
Silica modulus (SM), sometimes called silica ratio, is silica divided by the sum of alumina and iron oxide. It governs how much liquid phase forms in the kiln. High SM means less liquid, harder burning and more refractory wear.
Alumina modulus (AM), or alumina ratio, is alumina divided by iron oxide. It affects the liquid phase viscosity and the setting behaviour of the finished cement.
Quality control
Chemistry is monitored continuously, typically by X-ray fluorescence on sampled material, with automated control adjusting the feeders that proportion the raw materials. Raw mix chemistry drift is the most common upstream cause of clinker quality problems, and it shows up downstream as high free lime or low early strength before anyone looks at the mill.
Preheating and Calcination
The preheater tower and precalciner remove carbon dioxide from the limestone before the meal reaches the kiln, and in a modern plant they do 90 to 95 percent of that work.
A cyclone preheater is a vertical tower containing a series of cyclones through which raw meal falls counter-current to hot kiln exhaust gas. The meal is heated progressively as it descends while the gas cools as it rises, recovering heat that would otherwise go up the stack.
Calcination is the thermal decomposition of calcium carbonate into calcium oxide and carbon dioxide, occurring at approximately 900°C:
CaCO3 → CaO + CO2
A precalciner is a separate combustion chamber between the preheater and the kiln with its own fuel input, where the bulk of calcination occurs before the meal enters the rotary kiln. Moving calcination out of the kiln shortens the kiln, increases throughput and reduces fuel consumption.
Why this matters for emissions
Roughly 60 percent of a cement plant's CO2 comes from this reaction, not from fuel combustion. It is released by the chemistry of the limestone itself, which is why cement decarbonisation is a harder problem than fuel switching alone can solve.
The Kiln: What Happens at 1450°C
Clinker forms at approximately 1450°C, where 20 to 30 percent of the material partially melts and belite reacts with calcium oxide to produce alite.
The rotary kiln is an inclined steel cylinder lined with refractory brick, set at roughly a 3 degree slope and rotating slowly so that material travels down its length. Residence time in the kiln is typically 20 to 30 minutes.
The reaction sequence
The events inside the kiln occur in this order:
- Evaporation of free water
- Evolution of combined water in the argillaceous components
- Calcination of calcium carbonate to calcium oxide
- Reaction of CaO with silica to form dicalcium silicate
- Reaction of CaO with aluminium and iron-bearing constituents to form the liquid phase
- Formation of clinker nodules
- Evaporation of volatiles
- Reaction of excess CaO with dicalcium silicate to form tricalcium silicate
The temperature profile
A note on the flame. The combustion gas in the sintering zone reaches 1800 to 2000°C, but the material does not. The distinction matters, because a figure of 2000°C applied to clinker rather than to the flame is a common and serious error.
What leaves the kiln
Clinker exits as rounded nodules typically between 1 mm and 25 mm across, at 1300 to 1450°C.
Free lime is calcium oxide that did not combine during clinkering, and it is the primary indicator of burning quality. High free lime means the burning was incomplete or the chemistry was wrong, and it causes unsoundness, meaning delayed expansion in the hardened cement. It is measured on every clinker sample.
Cooling: Why Quench Speed Determines Strength
Clinker is quenched rapidly not for handling convenience but to preserve alite, which reverts to belite if cooling is slow.
Belite, dicalcium silicate or C2S, reacts above 1300°C to form alite, tricalcium silicate or C3S, the main source of early cement strength. If cooling is too slow, that reaction runs backwards. Alite decomposition into belite and free lime occurs between 900°C and 1250°C.
C3S → CaO + C2S
A plant that produces good clinker chemistry in the kiln and cools it slowly will ship cement with poor early strength and no obvious fault upstream.
The grate cooler
Clinker falls from the kiln outlet onto a moving grate through which cooling air is blown from below. Clinker entering typically has a temperature of 1300 to 1450°C and exits at around 100 to 150°C.
The heated air is recovered rather than discarded. It returns to the process as secondary air feeding the kiln burner and tertiary air feeding the precalciner, which is one of the largest fuel savings available in a cement plant.
Cooling rate
Conventional practice quenches clinker to around 200°C at rates exceeding 100°C per minute, with grate coolers commonly operating in the range of tens of degrees per minute depending on bed depth and air flow. The controlling requirement is to pass through the 1250°C to 900°C window quickly enough that alite is preserved.
Finish Grinding: Gypsum, Blaine and Energy
Clinker is ground with 3 to 5 percent gypsum, and without the gypsum the cement is unusable.
Gypsum controls setting time by regulating the hydration of tricalcium aluminate, C3A, which otherwise reacts almost instantly on contact with water. Without gypsum, cement flash sets and cannot be placed. It is added at the finish mill, not in the kiln, because it would decompose at clinkering temperature.
The mill
Grinding is performed in ball mills, vertical roller mills, roller presses, or combinations of these. A ball mill is a rotating horizontal cylinder charged with steel balls; clinker and gypsum enter one end and partially ground cement exits the other. Vertical roller mills grind between rollers and a rotating table and are generally more energy-efficient, which is why most new plants and expansions specify them.
Grinding aids
Small quantities of organic compounds are added to prevent powder agglomeration and coating of the ball charge and mill lining. Triethanolamine at around 0.1 wt% is common, along with ethylene glycol, oleic acid and dodecylbenzene sulphonate. These are process aids dosed at a tenth of a percent, not to be confused with gypsum at 3 to 5 percent.
Fineness: Blaine is the metric
Blaine specific surface area is the engineering measure of cement fineness, expressed in square centimetres per gram, and it is determined by air permeability under ASTM C204. Typical ordinary Portland cement runs in the region of 3,200 to 3,500 cm²/g, with high-early-strength cements ground finer, around 4,100 cm²/g.
The American Cement Association describes the resulting powder as approximately 150 billion grains per pound, which is a useful illustration and not a specification. Purchase orders and quality records use Blaine.
Blaine drives grinding energy directly. The higher the Blaine, the more energy required to grind the clinker and additives, which makes fineness a product specification with a direct operating cost consequence.
Packing, Dispatch and Cement Types
Finished cement is stored in silos and dispatched in bulk or in 20 to 40 kg bags, with bulk accounting for the large majority of volume in industrial markets.
Bulk cement moves by road tanker, rail and ship. Bagging serves smaller customers and markets where bulk handling infrastructure does not exist.
What the product is specified against
Under ASTM C150, Type I is general purpose, Type II offers moderate sulfate resistance, Type III provides high early strength through finer grinding and adjusted chemistry, Type IV is low heat of hydration, and Type V is high sulfate resistance. Specify the type against the exposure condition, not by habit.
Blended cements under ASTM C595 or the CEM II through CEM V designations in EN 197-1 replace a proportion of clinker with slag, fly ash, pozzolan or limestone. They lower cost and carbon intensity per tonne of cement, which is why they now dominate many markets.
Cement, concrete, and how hardening works
Cement is the binder. Concrete is the finished structural material formed when cement is combined with water, sand and coarse aggregate.
Cement hardens by hydration, a chemical reaction in which water reacts with the calcium silicate phases to form calcium silicate hydrate, conventionally written C-S-H, together with calcium hydroxide. C-S-H is the binding phase that develops compressive strength over time. The rate and ultimate strength depend on water-to-cement ratio, curing conditions, temperature and the clinker phase composition.
Dry Process and Wet Process
The dry process feeds the kiln a dry powder and the wet process feeds a slurry, and that single difference explains the entire energy gap between them.
In a wet process kiln, the raw meal typically contains approximately 36 percent moisture, all of which must be evaporated using kiln fuel before any useful reaction occurs. Wet kilns were developed to improve chemical uniformity in the raw meal, and the uniformity advantage no longer justifies the fuel penalty.
Dry process lines with preheater towers and precalciners are the current standard for new capacity. Heat is recovered from the kiln exhaust in the preheater and from the clinker in the cooler, and calcination occurs outside the kiln.
If you operate a wet line, the fuel consumption gap is not a maintenance problem and cannot be closed by tuning. It is inherent to the process route.
What Stops a Cement Kiln
Most cement plants run a single kiln line, which means a small number of large rotating assets are each capable of stopping the entire business.
This is the part no process guide covers, and it is the only part a plant manager acts on.
The auxiliary drive point
A hot rotary kiln must keep turning even when it is not producing, because a stationary kiln at temperature sags under its own weight and the shell distorts permanently. That is why kilns have auxiliary drives with independent power. Loss of both main and auxiliary drive on a hot kiln is among the most expensive failures in heavy industry.
Refractory
Refractory lining life and coating stability are the dominant planned-outage driver. Ring formation and build-up in the kiln, caused by chemistry or fuel changes, restricts material flow and can force an unplanned stop. Monitoring kiln shell temperature identifies coating loss before the shell is damaged.
What this means for maintenance strategy
A single-line plant cannot spread risk across redundant equipment, so criticality ranking and condition monitoring carry more weight here than in a multi-train facility. For matching monitoring strategy to failure mode and criticality, see our comparison of predictive versus preventive maintenance. For the PM regime on mills, fans and drives, see our rotating equipment field guide. For structuring the planned outage itself, see our outage planning guide.
Insurance and staffing
Machinery breakdown underwriters price a single-line plant differently from a multi-line one, and they assess condition monitoring and maintenance records directly. Staffing follows the same logic: a plant with no redundant train needs the capability to respond immediately, because there is nothing to switch to.
Energy and Power
Cement is among the most energy-intensive industries in the world, and the electrical load is continuous, large and concentrated in a few machines.
Finish grinding alone consumes 32 to 37 kWh per tonne in a modern ball mill, equivalent to 29 to 34 kWh per short ton. That is one stage. Raw grinding, the kiln drive, the ID fan, the preheater fans and the cooler fans sit on top of it.
The ENERGY STAR Guide for the Cement Industry documents these figures and the efficiency measures available against them.
Where the electricity goes
Grinding dominates, split between the raw mill and the cement mill. The fans are next, and they run continuously. The kiln drive itself is a smaller share than most people expect, because the kiln turns slowly.
Blaine is the lever most plants overlook. Grinding finer than the specification requires costs electricity every hour of every day for no product benefit.
Waste heat recovery
Kiln exhaust and cooler exhaust both carry recoverable heat, and waste heat recovery systems generating electricity from them are established technology in cement. The economics depend on the plant's electricity price and on how much heat is already recirculated to the preheater and precalciner.
Alternative fuels
Cement kilns can burn a wide range of alternative fuels including waste-derived fuels, biomass and tyres, because the long residence time and high temperature destroy organics and the clinker chemistry absorbs ash. Substitution reduces fuel cost and fossil CO2, and it constrains the chemistry, since ash composition enters the raw mix.
Captive generation
Where grid supply is unreliable or expensive, many cement plants operate their own generation. That is a power infrastructure decision with its own analysis, and for long-lead equipment procurement supporting it see our guide to the industrial procurement process.
ISO 50001, Energy management systems, provides the management framework where energy performance is formally managed.
Regulatory Framework
US cement plants are regulated by the Mine Safety and Health Administration rather than OSHA, and by a dedicated air emissions standard.
MSHA jurisdiction is the fact most people get wrong. Cement quarries and, in most configurations, the associated plant fall under MSHA regulation in 30 CFR, not under OSHA. That changes the inspection regime, the training requirements, the recordkeeping and the enforcement mechanism. Contractors working on site must be MSHA-trained, which is a prequalification requirement that catches out providers from other sectors.
Emissions
Cement CO2 has two distinct sources. Process emissions come from the calcination reaction itself, releasing CO2 chemically bound in the limestone, and account for roughly 60 percent of the total. Combustion emissions come from kiln and calciner fuel.
That split is why fuel switching alone cannot decarbonise cement, and why carbon capture, utilisation and storage is being pursued in this sector more seriously than in most. Manufacturers are implementing CCUS to address the process fraction that no fuel change can reach.
Emission control on the stack, principally for particulate matter, is standard on every modern line and is a continuous operating requirement rather than an add-on.
How Cement Operations Vary
The process is the same everywhere. What changes is the plant configuration and the standard the product is sold against.
Integrated plant versus grinding station
An integrated plant runs the full chain from quarry to dispatch. A grinding station imports clinker and grinds it with gypsum and supplementary materials. Grinding stations sit near markets rather than deposits, have no kiln, and therefore have a completely different reliability profile and a much lower capital cost.
Plant scale
A large integrated line has more buffer stock between stages and more capacity to absorb a short stoppage. A small plant has less of everything, which raises the relative value of condition monitoring and spares holding.
Regional standards
North American markets specify to ASTM C150, C595 or C1157. European and many international markets specify to EN 197-1 using the CEM designations. Confirm which applies before specifying, because the type numbering is not interchangeable between them.
Outside the United States
The chemistry, the equipment and the ASTM or EN standards are unchanged. The safety and emissions regimes are not. MSHA is a US framework, and other jurisdictions regulate quarrying and cement manufacture through their own mining and environmental authorities.
What Prismecs Does
Prismecs is an engineering and power services company working on the electrical, rotating equipment and control systems that industrial plants depend on.
Prismecs does not manufacture cement, design cement process lines or supply cement process equipment. What it delivers in heavy industrial environments is the layer underneath the process: O&M services for rotating and electrical assets, I&C services for control systems, power generation asset services, distributed energy solutions for on-site power, and EPCM services for project delivery.
Apply the same test to any provider working on your site. Ask whether their technicians are MSHA-trained. Ask what they have done on a single-line plant where there is nothing to switch to. Ask which of the seven assets above they have actually maintained.
To discuss reliability or power on a cement or minerals processing site, send your line configuration, your critical asset list and your current monitoring arrangement to sales@prismecs.com or call +1 (888) 774-7632.
Frequently Asked Questions
How is cement manufactured step by step?
Seven stages. Limestone and clay are quarried and crushed to about 6 inches then 3 inches. The materials are proportioned and ground into raw meal, dried below 1 percent moisture. A cyclone preheater and precalciner drive off CO2 at around 900°C. A rotary kiln forms clinker at approximately 1450°C. A grate cooler quenches it from 1300 to 1450°C down to 100 to 150°C. Clinker is ground with 3 to 5 percent gypsum, then stored and dispatched.
What temperature does clinker form at?
Approximately 1450°C. Between 1300 and 1450°C, 20 to 30 percent of the material partially melts and belite reacts with calcium oxide to form alite, and a peak temperature of 1400 to 1450°C is typically required to complete the reaction. The combustion gas in the sintering zone reaches 1800 to 2000°C, but the material itself does not approach that, and confusing the two is a common error.
Why is clinker cooled rapidly?
To preserve alite. Belite reacts above 1300°C to form alite, tricalcium silicate, which is the main source of early cement strength. If cooling is too slow that reaction reverses, with alite decomposing back into belite and free lime between 900°C and 1250°C. Rapid quenching through that window is what protects the strength the kiln just produced, not merely a handling convenience.
Why is gypsum added to cement?
To control setting time. Gypsum is interground with clinker at 3 to 5 percent by weight and regulates the hydration of tricalcium aluminate, C3A, which otherwise reacts almost instantly with water. Without gypsum the cement flash sets and cannot be placed or finished. It is added at the finish mill rather than in the kiln, because it would decompose at clinkering temperature.
What is the raw material for cement?
Limestone supplies calcium and makes up approximately 80 percent of the raw mix. Clay or shale supplies silicon, aluminium and iron and makes up the remaining 20 percent. Corrective materials including marl, sand, fly ash, mill scale, bauxite and iron ore are added in small quantities to trim the chemistry. Cement requires four oxides: calcium oxide, silica, alumina and iron oxide.
What are C3S, C2S, C3A and C4AF?
The four principal clinker phases in cement chemist notation. C3S is alite, tricalcium silicate, responsible for early strength. C2S is belite, dicalcium silicate, contributing later strength. C3A is tricalcium aluminate, very fast reacting and requiring gypsum control. C4AF is tetracalcium aluminoferrite, which acts as a flux lowering the kiln melting point. Bogue calculation estimates their proportions from the oxide analysis.
What is lime saturation factor?
LSF expresses how much calcium oxide is present relative to the maximum that the silica, alumina and iron in the mix can chemically combine with. Set too high, excess calcium oxide remains as free lime, causing unsoundness in the hardened cement. Set too low, alite formation is incomplete and early strength suffers. It is one of three control ratios alongside silica modulus and alumina modulus.
How is cement fineness measured?
By Blaine specific surface area, expressed in square centimetres per gram and determined by air permeability under ASTM C204. Ordinary Portland cement typically runs around 3,200 to 3,500 cm²/g, with high-early-strength cements ground finer at around 4,100 cm²/g. The higher the Blaine, the more grinding energy consumed, which makes fineness a specification decision with a direct electricity cost.
How much energy does cement grinding use?
Finish grinding in a modern ball mill consumes 32 to 37 kWh per tonne, equivalent to 29 to 34 kWh per short ton. That is one stage of the process. Raw grinding, the kiln drive, the ID fan, preheater fans and cooler fans are additional. Grinding dominates a cement plant's electricity consumption, which makes Blaine specification and mill efficiency the largest electrical levers available.
What is the difference between the dry process and the wet process?
The dry process feeds the kiln a dry powder; the wet process feeds a slurry. Wet process raw meal typically contains approximately 36 percent moisture, all of which must be evaporated using kiln fuel before useful reaction begins. That single difference explains the entire energy gap. Wet kilns were developed for better raw meal uniformity, an advantage that no longer offsets the fuel penalty.
What actually stops a cement kiln?
Seven assets, on most plants running a single line. The kiln main drive, the induced draught fan, the preheater and cooler fans, the raw mill, the cement mill, the crushers, and the kiln refractory. A hot kiln must keep rotating even when not producing, because a stationary hot kiln sags under its own weight and the shell distorts permanently, which is why auxiliary drives exist.
Which regulator governs US cement plants, MSHA or OSHA?
The Mine Safety and Health Administration, under 30 CFR, regulates cement quarries and in most configurations the associated plant, rather than OSHA. That changes inspection, training, recordkeeping and enforcement. Contractors working on site must be MSHA-trained, which is a prequalification requirement that frequently catches out service providers whose experience comes from OSHA-regulated sectors.
What air emissions regulations apply to cement plants?
40 CFR Part 63 Subpart LLL, the NESHAP for the Portland Cement Manufacturing Industry and commonly called the Portland Cement MACT, governs hazardous air pollutants. 40 CFR Part 60 Subpart F sets new source performance standards for Portland cement plants. Roughly 60 percent of cement CO2 comes from calcination of the limestone itself rather than fuel, which is why fuel switching alone cannot decarbonise the process.
What is the difference between cement and concrete?
Cement is the binding agent, a fine powder produced by grinding kiln clinker with gypsum. Concrete is the structural material formed when cement is combined with water, sand and coarse aggregate. Cement hardens through hydration, in which water reacts with the calcium silicate phases to form calcium silicate hydrate, written C-S-H, together with calcium hydroxide. C-S-H is the phase that develops compressive strength.
Tags: Cement Manufacturing Process Clinker Production Kiln Reliability Cement Plant Energy Portland Cement Standards
recent posts
Power Utilities
20 minutes read
Fast-Track Power Plants Deployment: How to Reach Speed to Power in Under 12 Months
Fast-track power plant deployment can hit first power in weeks. See real TM2500 timelines from permitting to COD, proven in Oman and Taiwan. Plan your...
O&M Services
11 minutes read
Gas Turbine Outage Planning: Schedule, Scope Rules, and Checklist
Gas turbine outage planning starts 18 months out. Get the T-minus schedule, scope freeze rules, parts readiness gates and checklist. Talk to a Prismec...
O&M Services
15 minutes read
Predictive vs Preventive Maintenance: How to Choose Per Asset
Most plants apply predictive vs preventive maintenance facility wide and overspend. Match each asset by failure mode, criticality and P-F interval. Ta...
Data Centers
59 minutes read
Data Center Power Redundancy: N, N+1, 2N and 2N+1- What Each Level Takes to Build and Prove
Most data center power redundancy claims fail under test. See what N+1, 2N and 2N+1 truly require, how Level 5 testing proves them, and what to demand...