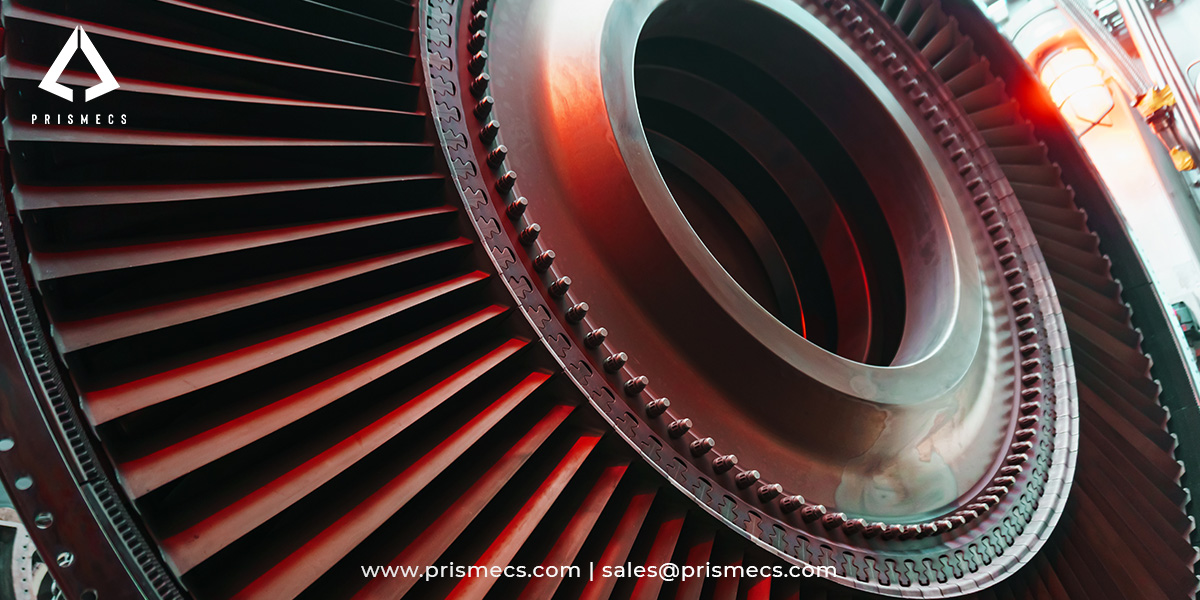
A turbine lubrication system has two jobs. It keeps the bearings alive, and it reports on their condition continuously.
Most operators treat the first as the system and the second as paperwork. The second is where the warning comes from. Ferrous debris on a chip detector, a wear metal trend in a spectrographic analysis, or a rising acid number will indicate a developing problem weeks or months before vibration or temperature alarms respond.
The system is also specified equipment, not just plumbing. API Standard 614, Sixth Edition, February 2022 governs its design in petroleum, chemical and gas service, and the Sixth Edition changed how lube pumps are sized in a way that matters on hot sites.
This guide covers what the system does, what it contains, how to specify it, and how to read what it is telling you.
What the Lubrication System Does
A turbine lubrication system delivers clean, cool oil at controlled pressure to the bearings, and removes the heat those bearings generate.
Four functions, and the order is not the order most people assume:
Thermal management. Oil circulates around high-speed bearings to dissipate heat, preventing overheating and maintaining efficiency. On a large machine, cooling consumes more of the oil flow than lubrication does. The film that separates the surfaces is thin; the flow required to carry away the heat is not.
Friction reduction. The oil film separates rotating and stationary surfaces so they do not contact, reducing wear and extending turbine life.
Pressure stabilisation. Consistent oil pressure under varying load is what maintains that film. Pressure loss means metal contact in seconds.
Operational resilience. Reliable lubrication is what keeps a machine from a forced outage, and lubrication failures are among the most expensive because they damage the bearings rather than tripping the unit cleanly.
The function most pages omit
Turbine lubricants are expected to serve as both lubricating oil and hydraulic fluid, supplying the turbine, the generator, the gear unit and auxiliary components from one system.
That has a consequence this article returns to later. Deposits that would be cosmetic in a bearing are operational in a control valve, because the same oil operates the hydraulics.
Effective lubrication directly affects capital and operating cost, through maintenance intervals, downtime risk and output.
Wet Sump and Dry Sump
Industrial gas turbines use one of two lubrication architectures, and the choice follows machine size and thermal control requirements.
A wet-sump system stores oil within the turbine assembly itself, enabling rapid circulation to bearings and moving components. It is simpler, has fewer external components and suits smaller industrial turbines and fast-start backup units, with straightforward maintenance workflows.
A dry-sump system stores oil in an external reservoir separate from the machine. Scavenge pumps return oil from the bearing housings to the reservoir and pressure pumps supply it back out.
Dry sump is the architecture on large industrial and utility turbines because the external reservoir allows precise thermal control, proper deaeration, far better oil management, and reliable circulation under high load or extreme ambient conditions. It enhances component longevity, operational reliability and turbine availability, which is why industrial plants, independent power producers and utility operators specify it.
The practical difference
Dry sump gives you access. The reservoir can be sampled, inspected, filtered offline and treated without opening the machine. On a wet sump, the oil condition and the machine condition are the same inspection.
The Pressure and Scavenge Circuits
Every dry-sump lubrication system has two circuits moving in opposite directions, and confusing them makes the rest of the system unreadable.
The pressure circuit takes oil from the reservoir, raises it to supply pressure, cools it, filters it and delivers it to the bearing headers. Everything in it is about delivering oil in a controlled condition.
The scavenge circuit returns oil from the bearing housings to the reservoir. It handles a mixture of oil and air, which is why scavenge pumps are sized for substantially greater volumetric capacity than pressure pumps.
Scavenge pumps are typically positive displacement and frequently one per bearing compartment. That arrangement matters diagnostically, for reasons covered in the chip detector section below.
The reservoir sits between the two circuits and does more than store oil. It provides residence time for entrained air to separate and for water and heavy particulate to settle out.
The Components
A turbine lubrication system comprises twelve components, and the four most commonly listed are not the four most likely to cause an outage.
The reservoir
Beyond storage, it provides expansion space allowing oil to expand as it absorbs heat from bearings and gears. Many reservoirs include a deaerator tray, which separates entrained air from the oil returned to the upper part of the tank by the scavenge system.
Deaeration is not optional. Aerated oil compresses, which means the bearing film becomes variable, and it also accelerates oxidation.
Pumps
The main pump is usually driven from the machine shaft, which is efficient and means it stops when the machine stops. That single fact is why emergency lubrication exists, and it is covered in the next section.
Gear-type pumps combining a pressure section and a scavenging section are common. On larger systems, rotary screw and centrifugal pumps appear, each with its own sizing constraints under API 614.
Filters
Filters remove contaminants and prevent wear of bearings and journals. Oil flows from the outer casing into the filter body, and elements are either laminated paper, which is replaceable, or stainless steel mesh, which is durable and cleanable.
Specify duplex filters with a transfer valve so elements can be changed with the machine running. A simplex filter on a continuously operating machine means an outage to change an element.
Pressure relief valve
The relief valve prevents excessive pressure buildup, returning excess oil to the pump inlet when pressure exceeds the preset limit. It is critical on machines with integrated oil coolers, because it protects the cooler's thin-walled construction from overpressure.
For spares strategy on these components, see our guide to turbine spare parts management. For the wider component picture, see our gas turbine parts guide.
Emergency Lubrication and Coastdown
When a turbine trips, the rotor keeps spinning for minutes while the shaft-driven main pump stops delivering, and that window is where bearings are destroyed.
Coastdown is the period between trip and standstill. The rotor still carries its full weight on the bearings, still needs an oil film, and the pump that was providing it has stopped.
Emergency lubrication is what covers the gap. Dedicated emergency pumps, electrically or diesel driven, or stored-pressure accumulators, provide oil flow if the main pumps fail, protecting bearings during coastdown.
The three-layer arrangement
The AC auxiliary pump, motor-driven from the plant supply, starts on low lube oil pressure and covers normal starts, shutdowns and main pump unavailability.
The DC emergency pump, supplied from the station battery, covers loss of AC supply. This is the layer that matters during a station blackout, and it is the reason the battery system is part of the turbine's protection rather than a facilities item.
The accumulator maintains pressure during the seconds between loss of one source and the other starting. Dynamic analysis is used to confirm whether an accumulator is required on a given API 614 system.
Jacking oil
A jacking oil pump supplies high-pressure oil to lift the rotor off the bearings before the machine is turned on turning gear, preventing boundary lubrication during slow rotation. On many installations it also supplies the hydraulic motor that drives the turning gear.
The hydraulic fuse
On some designs a hydraulic fuse is fitted between the main oil supply and the emergency system, to block the connection if the emergency system itself develops a leak. Without it, a leak in the backup drains the primary.
If the emergency pump does not start
This is the failure mode behind a large proportion of catastrophic bearing damage. The pump is proved by testing, not by its presence on the P&ID. Monthly start testing of the AC auxiliary and DC emergency pumps, plus battery capacity testing, belong in the preventive maintenance programme.
Documented practice includes cases where a turbine avoided bearing failure precisely because the automatic emergency pump started on main pump trip and maintained bearing flow through coastdown. That outcome depends entirely on whether the pump was last proved.
For what wiped and damaged bearings actually look like and why, see our analysis of gas turbine bearing failure causes.
Oil Specification: Grade and Type
Turbine oils are specified by ISO viscosity grade, and the two in common industrial use are ISO VG 32 and ISO VG 46.
ISO grades 32, 46 and 68 are the products of interest in the turbine industry, with grades 46, 68 or 77 used where the turbine manufacturer specifies higher viscosity. ISO VG 32 and 46 are the two most commonly used on industrial gas turbine lubrication systems.
ISO 8068 governs turbine oil specification, alongside the turbine OEM's own requirements.
Choosing between 32 and 46
Lower viscosity gives lower churning losses and better cold-start behaviour. Higher viscosity gives a thicker film at elevated temperature. The selection is the OEM's, and deviating from it affects warranty position, which makes it a specification question rather than a procurement preference.
On hot sites, confirm the grade against the actual oil supply temperature, not against the datasheet ambient. Viscosity falls with temperature, and the film thickness that matters is the one at operating condition.
Mineral and synthetic
Industrial frame machines predominantly use highly refined mineral turbine oils. Aeroderivative machines frequently require synthetic esters, because the bearing temperatures in an aero-derived core exceed what mineral oil tolerates.
These are not interchangeable. Mixing them, or topping up one with the other, is a compatibility problem rather than a dilution.
Cleanliness: The ISO 4406 Target
Turbine oil cleanliness is specified as an ISO 4406 code, and most turbine OEMs target between ISO 15/13/10 and ISO 17/15/12.
ISO 4406 defines cleanliness codes based on particle counts per millilitre at 4, 6 and 14 microns, expressed as three scale numbers. Lower numbers mean cleaner oil, and each step represents a doubling of particle count.
What OEMs actually specify
Published OEM cleanliness tables show new oil specified at ISO 4406 16/14/12 for both ISO VG 32 and ISO VG 46 on several industrial gas turbine platforms, with some specifications setting a minimum standard of 20/17/14.
Some OEMs additionally require that oil be filtered through a 10 micron filter before entering service.
API 614 Annex E carries the allocation of ISO 4406 scale numbers, alongside SAE AS4059 cleanliness classes for differential particle counts, a relative size comparison of common particle materials, and typical dynamic film thickness for different equipment types.
Why the film thickness comparison matters
That last item is the reason cleanliness is specified so tightly. A particle larger than the oil film passes through the bearing clearance by removing material. When the dynamic film is measured in microns, particles measured in microns are not contaminants in a general sense; they are abrasives.
What to specify
The ISO 4406 target code at a named sampling point. The filtration rating and beta ratio, which expresses filter efficiency at a stated particle size. New oil cleanliness on delivery, which is frequently worse than the in-service target and requires filtration before filling.
If cleanliness drifts out of specification
Find the ingress source rather than increasing filtration. Common sources are make-up oil added without filtration, breather failure allowing airborne dust, water ingress, and internal wear. Filtering harder treats the symptom and accelerates the element spend.
Varnish: The Modern Problem
Varnish is a thin, insoluble deposit of oxidised oil degradation products that forms on valve spools, bearing surfaces and heat exchanger plates, and it is invisible to conventional particle counting.
It is a different problem from particulate contamination. Varnish precursors are dissolved in the oil at operating temperature and deposit out as the oil cools, which means a particle count can be perfect while varnish is accumulating.
Why it matters operationally
Because turbine oil is also hydraulic fluid. Varnish on a servo valve spool causes sticking, slow response or failure to stroke, which on a fuel control or an inlet guide vane actuator is a unit trip rather than a maintenance finding.
Varnish on heat exchanger plates reduces cooling capacity, which raises oil temperature, which accelerates oxidation. It is self-reinforcing.
How it is detected
Membrane patch colorimetry (MPC), ASTM D7843, is the standard test. Oil is filtered through a membrane patch and the colour of the deposit is measured. High MPC values indicate elevated varnish risk.
RULER, remaining useful life evaluation routine, measures remaining antioxidant additive, which indicates how much oxidation protection the oil still has.
Add MPC to the oil analysis programme if it is not already there. On modern highly refined base oils it is the test most likely to find a developing problem that particle count and viscosity will miss.
What the Oil Is Telling You
Oil condition is the earliest indicator of a developing bearing problem, and it reports weeks to months before vibration or temperature alarms respond.
The analysis set
Trend matters more than any single result. A wear metal value within limits that has doubled in two samples is a finding; the same value flat for a year is not.
Wear metals identify the component
Different components are made of different alloys, so the metal in the oil identifies the source. Babbitt bearings release tin and lead. Steel components release iron. Bronze cages and bushings release copper. A rising tin and lead trend points at bearing material; a rising iron trend points at something harder.
Chip detectors and debris monitors
A chip detector is a magnetic probe in the oil path that captures ferrous debris. An oil debris monitor (ODM) reports the quantity and size distribution of that debris continuously rather than at inspection.
The diagnostic value comes from where the detector sits. Where debris collection devices are fitted per scavenge pump and per bearing compartment, a finding at one device identifies which bearing compartment produced it, and therefore which bearing is degrading.
That converts a warning into a diagnosis. A single detector on a common return tells you the machine has a problem; per-compartment detection tells you which bearing to inspect.
Sampling discipline
Sample from the same point, in the same way, at the same operating condition each time, or the trend is noise. New oil should be tested on receipt for specification compliance, because delivered cleanliness is frequently worse than the in-service target.
For how this fits a condition-based maintenance strategy and where it sits against other monitoring methods, see our comparison of predictive versus preventive maintenance. For the task-level programme, see our rotating equipment maintenance field guide.
API 614 and How to Specify the System
API Standard 614, Sixth Edition, February 2022, Lubrication, Shaft-sealing, and Oil-control Systems and Auxiliaries, is the governing specification standard for these systems in petroleum, chemical and gas service.
It covers the minimum requirements for lubrication systems, oil-type shaft-sealing systems, oil-control systems and auxiliaries, and it provides typical piping and instrumentation diagrams and module options for each sub-system.
The scope boundary, which is frequently got wrong
API 614 excludes dry gas seal systems and fuel systems.
For dry gas seal systems, refer to API 692. For high-pressure oil systems and fuel systems used on gas turbines, refer to API 616.
Specifying API 614 for a scope that includes fuel systems gets you a quotation for something narrower than you asked for, and the gap appears at commissioning.
The pump sizing change that matters
Texas A&M Turbomachinery Laboratory documents a specification change between editions that affects hot-site installations directly.
API 614 Fifth Edition specified that positive displacement lube oil pumps be sized for lowest oil viscosity. The Sixth Edition stipulates that each pump be capable of supplying the normal oil flow required at the pressure-limiting valve set pressure and at minimum viscosity, where minimum viscosity means the viscosity corresponding to the highest oil temperature at the pump suction, plus the heat rise through the pump itself.
That is a stricter and more realistic basis. A pump sized to the older basis can be marginal at the temperature it will actually see on a hot site in summer.
Rotary screw pumps must be sized so that the pressure differential through the pump is not greater than 90 percent of the manufacturer's rating at rated capacity and minimum viscosity.
On centrifugal pumps, applying the conventional 10 percent continuous head rise from rated point to shut-off can destabilise the lube oil pressure controller, because a small flow change produces a relatively large discharge pressure change.
What to require in a specification
The configuration code and sub-system scope. The ISO VG grade and the oil type. The ISO 4406 cleanliness target with the sampling point. Filtration rating and beta ratio. Pump arrangement including auxiliary and emergency provision, with the sizing basis stated. Instrumentation with alarm and trip setpoints. Reservoir retention time. And the vendor data document requirements, which API 614 specifies in detail.
Outside the petroleum industries
IOGP S-744 is a supplementary specification to API 614 Sixth Edition, defining a minimum common requirement set for procurement of lubrication and oil-control systems in petroleum and natural gas industries. It adds documented checks including lube oil system heat-up time and provision for continued cool-down oil flow during isolation of driven equipment.
API standards apply internationally. Where a project works to IEC or national conventions instead, confirm which governs before the specification is issued.
Failure Modes and What They Mean
Five lubrication failures account for most lube-related turbine damage, and each has a signature before it has a consequence.
Low oil pressure. Pump failure, relief valve passing, filter blockage or a leak. The response window is seconds, which is why low pressure trips the machine and why the emergency pump must start automatically.
High oil temperature. Cooler fouling, temperature control valve failure, loss of cooling medium, or a bearing generating more heat than it should. Rising supply temperature with no change in ambient or load points at the cooling circuit; rising return temperature from one bearing points at that bearing.
Water ingress. From cooler tube leaks, seal leakage or condensation in the reservoir. Water destroys the oil film, promotes corrosion and accelerates additive depletion.
High filter differential pressure. The element is doing its job and is approaching capacity, or something upstream is generating debris. Change the element and investigate the cause, because a rapidly loading filter is a symptom.
Oil starvation. The most destructive and the fastest. Loss of supply for seconds at speed wipes bearing material. The usual causes are pump failure without emergency backup, a blocked supply line, or loss of suction from a low reservoir level.
Alarm and trip setpoints
Low lube oil pressure alarm, low-low pressure trip, high oil temperature alarm and trip, high filter differential pressure alarm, low reservoir level alarm, and emergency pump auto-start on low pressure. Setpoints are OEM-specific and should be verified against the manual rather than inherited from a previous machine.
Insurance, warranty and reporting
Machinery breakdown insurers assess lubrication maintenance records and oil analysis history when pricing and when settling claims. An undocumented oil programme is a claim problem after a bearing failure. Lube-related outages are reportable as forced outages and feed the forced outage rate used in capacity markets and O&M contracts. See our guide to power plant O&M metrics and contracts.
For structured root cause work after an event, see our guide to gas turbine troubleshooting and unplanned downtime, and for scheduling the intervention, our outage planning guide.
Frame, Aeroderivative and Steam
The architecture is common. The oil, the temperatures and the maintenance model are not.
Heavy-duty frame gas turbines use dry-sump systems with large external reservoirs, mineral turbine oils at ISO VG 32 or 46, and the oil typically serving hydraulic control functions as well as lubrication.
Aeroderivative gas turbines run higher bearing temperatures from their aero-engine cores and frequently require synthetic ester oils rather than mineral. Reservoirs are smaller and the system is more compact. Module exchange maintenance means the lube system and the gas generator are serviced on different cycles.
Steam turbines share the architecture and add the jacking oil and turning gear requirement prominently, since a hot steam turbine rotor must be rotated continuously to avoid bowing.
Oil and gas sites add hazardous area classification to electrical component selection, and frequently add dust or salt ingress to the reservoir breathing arrangement.
For compressor-side degradation that shows up in the same performance data, see our guides to gas turbine casings, clearance and fouling and compressor stall and surge.
What Prismecs Does
Prismecs operates and maintains gas turbine plant, supplies equipment and components, and provides installation, commissioning and controls support.
Delivered project scope includes four TM2500 units totalling 110 MW at Duqm, Oman, kept grid-ready with resident O&M crews, CMMS and parts support; eight TM2500 dual-fuel units totalling 260 MW at Birr, Switzerland, online in six months with a new 220 kV interconnection; an LM2500XPRESS plant at Miaoli, Taiwan delivered in ten months; three LM6000PC units adding 150 MW of fast-start reserve; and an LM6000 fleet decommissioned in Norway, transported and recommissioned at a new site.
The TM2500, LM2500 and LM6000 are aeroderivative machines, which is the class where synthetic ester lubricants and compact lube systems apply.
Capability spans O&M services for the operating phase, power generation asset services for the equipment, ready-to-ship equipment inventory for components and spares, I&C services for instrumentation and controls, supply chain solutions for procurement, and EPCM services for project delivery.
Prismecs is OEM-agnostic, which matters on lubrication because the party recommending an oil change interval or a component replacement is not the party selling the oil or the part.
Apply this article's criteria to any provider, including us. Ask which ISO 4406 target the system will be held to and at which sampling point. Ask whether MPC is in the oil analysis set. Ask how often the DC emergency pump is start-tested. Ask which API standard the system was specified against.
To discuss lubrication system condition, component supply or an O&M scope, send your machine model, oil grade and type, most recent oil analysis results and the symptom you are seeing to sales@prismecs.com or call +1 (888) 774-7632.
Frequently Asked Questions
What does a gas turbine lubrication system do?
It delivers clean, cool oil at controlled pressure to the bearings and removes the heat they generate. On a large machine, cooling consumes more of the oil flow than lubrication does, because the separating film is thin while the heat load is not. Turbine oil also typically serves as hydraulic fluid for the turbine, generator, gear unit and auxiliary components, which is why oil condition affects control response as well as bearing life.
What is the difference between wet sump and dry sump?
A wet-sump system stores oil within the turbine assembly, is simpler, and suits smaller industrial turbines and fast-start backup units. A dry-sump system stores oil in an external reservoir with scavenge pumps returning it from the bearing housings. Dry sump allows precise thermal control, proper deaeration and better oil management, which is why large industrial and utility turbines use it.
What is the pressure circuit and the scavenge circuit?
The pressure circuit takes oil from the reservoir, raises it to supply pressure, cools it, filters it and delivers it to the bearing headers. The scavenge circuit returns oil from the bearing housings to the reservoir and handles an oil and air mixture, which is why scavenge pumps are sized for greater volumetric capacity than pressure pumps. Scavenge pumps are frequently fitted one per bearing compartment.
Why does a turbine need an emergency lube oil pump?
Because the main pump is usually shaft-driven and stops when the machine stops, while the rotor keeps turning for minutes during coastdown. During that window the bearings still carry full rotor weight and still need an oil film. Dedicated emergency pumps, electrically or diesel driven, or stored-pressure accumulators provide flow if the main pumps fail, protecting bearings through coastdown.
What is the difference between the AC auxiliary and DC emergency pump?
The AC auxiliary pump is motor-driven from the plant supply and covers normal starts, shutdowns and main pump unavailability. The DC emergency pump is supplied from the station battery and covers loss of AC supply, which is the layer that matters during a station blackout. An accumulator maintains pressure during the seconds between one source stopping and the next starting.
What is a jacking oil pump?
A pump supplying high-pressure oil to lift the rotor off its bearings before the machine is rotated on turning gear, preventing boundary lubrication during slow rotation when hydrodynamic film cannot form. On many installations it also supplies the hydraulic motor driving the turning gear itself. It is particularly important on steam turbines, where a hot rotor must be turned continuously to avoid bowing.
Which ISO viscosity grade should a turbine use?
ISO VG 32 and ISO VG 46 are the two grades in common industrial turbine use, with 68 and occasionally 77 where the OEM specifies higher viscosity. ISO 8068 governs turbine oil specification alongside OEM requirements. The selection belongs to the turbine manufacturer, and deviating from it affects warranty position. On hot sites, confirm the grade against actual oil supply temperature rather than datasheet ambient.
Is mineral or synthetic turbine oil required?
It depends on the machine. Heavy-duty industrial frame turbines predominantly use highly refined mineral turbine oils. Aeroderivative machines frequently require synthetic ester oils, because bearing temperatures in an aero-derived core exceed what mineral oil tolerates. The two are not interchangeable, and topping up one with the other is a compatibility problem rather than a dilution.
What ISO 4406 cleanliness target should I specify?
Most turbine OEMs specify targets between ISO 15/13/10 and ISO 17/15/12. Published OEM tables show new oil specified at ISO 4406 16/14/12 for both ISO VG 32 and 46 on several industrial platforms, with some specifications setting a minimum of 20/17/14, and some requiring filtration through a 10 micron filter before service. ISO 4406 codes count particles per millilitre at 4, 6 and 14 microns.
Why does oil cleanliness matter so much?
Because the oil film separating bearing surfaces is measured in microns, and a particle larger than the film passes through the clearance by removing material. API 614 Annex E publishes typical dynamic film thickness alongside relative particle size comparisons for exactly this reason. At those dimensions, particles are not contaminants in a general sense; they function as abrasives in the load zone.
What is varnish and how is it detected?
Varnish is a thin, insoluble deposit of oxidised oil degradation products that forms on valve spools, bearing surfaces and heat exchanger plates. It is invisible to particle counting because precursors are dissolved at operating temperature and deposit as oil cools. It is detected by membrane patch colorimetry, ASTM D7843, with high MPC values indicating elevated risk, or by RULER testing of remaining antioxidant.
Why is varnish an operational problem rather than a cleanliness one?
Because turbine oil also serves as hydraulic fluid. Varnish on a servo valve spool causes sticking, slow response or failure to stroke, which on a fuel control or inlet guide vane actuator produces a unit trip rather than a maintenance finding. Varnish on heat exchanger plates also reduces cooling capacity, raising oil temperature and accelerating further oxidation.
What does a chip detector finding tell me?
That ferrous debris is being generated somewhere in the machine. The diagnostic value depends on placement: where debris collection devices are fitted per scavenge pump and per bearing compartment, a finding at one device identifies which compartment produced the debris and therefore which bearing is degrading. A single detector on a common return indicates a problem without localising it.
Which standard governs gas turbine lubrication system design?
API Standard 614, Sixth Edition, February 2022, Lubrication, Shaft-sealing, and Oil-control Systems and Auxiliaries. It covers lubrication, oil-type shaft-sealing and oil-control systems and auxiliaries, and provides typical P&IDs and module options. It excludes dry gas seal systems, which fall under API 692, and fuel systems and high-pressure oil systems on gas turbines, which fall under API 616.
How are lube oil pumps sized under API 614?
The Sixth Edition stipulates that each pump be capable of supplying the normal oil flow required at the pressure-limiting valve set pressure and at minimum viscosity, meaning the viscosity at the highest oil temperature at pump suction plus heat rise through the pump. The Fifth Edition had sized positive displacement pumps for lowest oil viscosity. Rotary screw pumps must run at no more than 90 percent of the manufacturer's rated pressure differential.
Tags: Gas Turbine Lubrication Turbine Oil Analysis API 614 ISO 4406 Cleanliness Turbine Bearings
recent posts
Power Utilities
20 minutes read
Fast-Track Power Plants Deployment: How to Reach Speed to Power in Under 12 Months
Fast-track power plant deployment can hit first power in weeks. See real TM2500 timelines from permitting to COD, proven in Oman and Taiwan. Plan your...
O&M Services
11 minutes read
Gas Turbine Outage Planning: Schedule, Scope Rules, and Checklist
Gas turbine outage planning starts 18 months out. Get the T-minus schedule, scope freeze rules, parts readiness gates and checklist. Talk to a Prismec...
O&M Services
15 minutes read
Predictive vs Preventive Maintenance: How to Choose Per Asset
Most plants apply predictive vs preventive maintenance facility wide and overspend. Match each asset by failure mode, criticality and P-F interval. Ta...
Data Centers
59 minutes read
Data Center Power Redundancy: N, N+1, 2N and 2N+1- What Each Level Takes to Build and Prove
Most data center power redundancy claims fail under test. See what N+1, 2N and 2N+1 truly require, how Level 5 testing proves them, and what to demand...