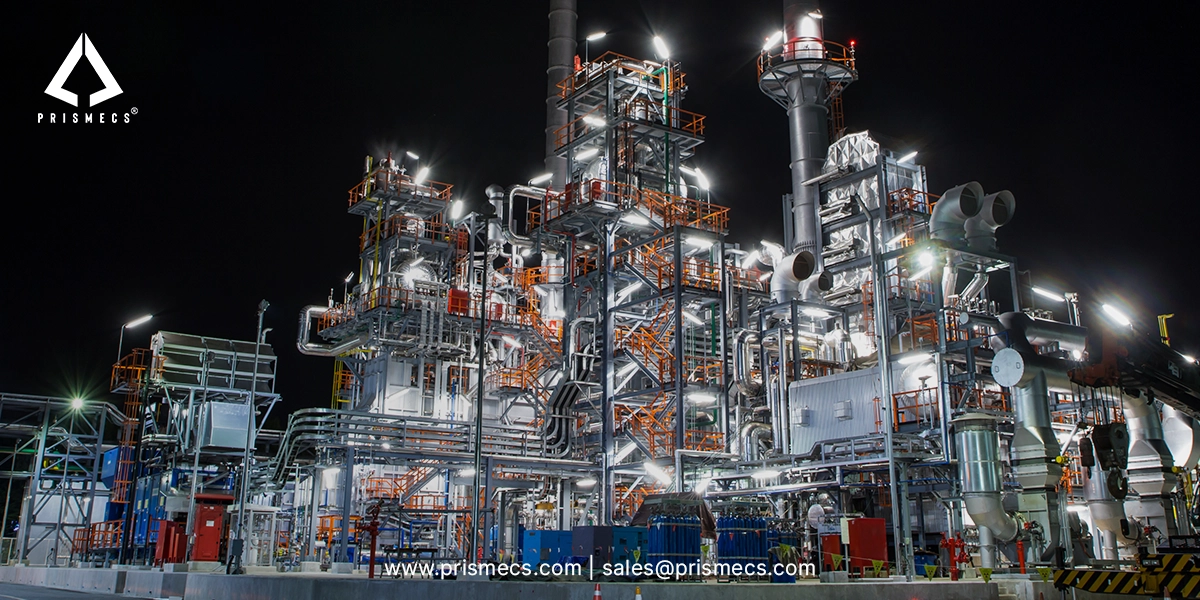
A petrochemical plant's output is set by its furnaces, and its availability is set by three things that have nothing to do with chemistry.
Steam cracking furnaces run 20 to 60 days before coke deposits force a shutdown for decoking, and each decoke cycle takes 1 to 3 days. On a furnace-limited plant, that rhythm sets the production schedule.
The cracked gas compressor compresses the entire product stream, and no spare exists. The utilities system supplies steam, power, cooling water and instrument air to every unit, so an interruption trips the complex rather than one line.
Everything else, including the chemistry, is scheduled around those three.
This guide explains how a petrochemical plant is structured, what each unit actually depends on, the codes that govern its mechanical integrity, and where its availability is won or lost.
What Is a Petrochemical Plant?
A petrochemical plant is a highly engineered industrial facility designed to process hydrocarbons such as ethane, propane, naphtha, and natural gas liquids into high-value chemical products at scale. These facilities operate through tightly controlled thermal, chemical, and mechanical processes that require advanced equipment integration, instrumentation, and operational expertise.
Most petrochemical plants are located near petroleum refineries or integrated into large petrochemical complexes. This configuration enables efficient feedstock transfer, shared utilities, and optimised production workflows.
What that integration actually means operationally
Shared utilities mean shared failure modes. A steam header, a cooling water system or an electrical bus serving both the refinery and the chemical complex creates a dependency that neither site controls alone.
Successful petrochemical operations depend not only on chemical reactions but also on plant reliability, process automation, and lifecycle asset management to maintain consistent output and safety standards. Those three are what the rest of this article covers.
How Petrochemical Plants Are Structured

Petrochemical plants are structured into key operational units, starting with feedstock preparation, followed by steam cracking, separation, and conversion processes. Each unit operates in sequence, transforming raw materials such as ethane, propane, or naphtha into valuable petrochemical products including ethylene and propylene.
The sequence matters for a reason beyond process flow. Each unit is a constraint on the one after it, which is why a plant is usually described as furnace-limited, compression-limited or separation-limited depending on which stage caps output.
Feedstock Preparation Units
Every petrochemical process starts with the feedstock. Operators select ethane, propane, naphtha, or natural gas liquids depending on the desired product slate and the prevailing price spread between them.
Natural gas liquids are the heavier hydrocarbons separated from natural gas, principally ethane, propane, butane and natural gasoline. These feedstocks come either directly from oil refineries or from natural gas processing plants.
At this stage the raw hydrocarbons are separated and purified to meet process specification. Off-specification feed does not simply reduce yield; contaminants accelerate coking in the furnaces downstream and shorten run length.
Steam Cracking Units
Steam cracking is the core operation, heating ethane, propane or naphtha with steam to break molecular bonds and produce ethylene and propylene.
Cracked hydrocarbon leaves the furnace radiant coils at a coil outlet temperature typically between 750 and 850°C, with naphtha crackers running at least 820°C. The hottest coil surface temperature reaches 1035 to 1180°C.
Coil outlet temperature, or COT, is the governing control parameter. Raising it increases conversion and ethylene yield, and it also increases coking rate sharply.
Manufacturers use ethylene to produce polyethylene, ethylene oxide, and other derivatives. Propylene is essential for creating polypropylene, acrylonitrile, and propylene oxide. The steam cracking unit also produces byproducts including butadiene, benzene, toluene, and xylene.
Run length and decoking: the plant's operating rhythm
Coke deposits on the inside of the radiant coils during cracking, progressively restricting flow and raising tube metal temperature. Steam cracking furnaces normally operate 20 to 60 days before a decoke operation is required.
Decoking isolates the furnace and passes steam or a steam and air mixture through the coils at 850 to 950°C, oxidising the coke until carbon dioxide concentration confirms the coil is clean.
A full decoke cycle typically takes 1 to 3 days and adds thermal cycling to the furnace. Every decoke removes production capacity from a furnace-limited plant.
Why decoke duration matters as much as run length
On a furnace-limited plant, where the cracker section caps overall ethylene output, hours spent decoking are hours of lost capacity. Cutting hours from each cycle recovers capacity almost as effectively as extending the run.
Two furnaces of the same design at the same plant can run cycles that differ by several hours, and the same furnace can run faster or slower from one decoke to the next. The binding constraint varies: tube metal temperature on one furnace, coil pressure drop on another, transfer line exchanger fouling on a third.
That variability is why fixed decoke schedules waste capacity. The schedule should follow the measured constraint rather than the calendar.
Coil life
Anti-coking coil technologies roughly double run length, from about 30 days uncoated to up to 60 days coated, with one commercial trial extending a 33-day run length substantially further. Ethylene furnace coil service life runs to around 14 years depending on operating conditions, decoking practice and alloy selection.
Separation and Recovery
After cracking, the mixture contains a range of gases and hydrocarbons that must be separated by fractionation, compression and cryogenic distillation.
Cracked gas is quenched rapidly to 338 to 510°C in a transfer line exchanger to stop the cracking reaction, then cooled further in a water quench tower operating at 35 to 40°C. On liquid feedstock plants, a prefractionator precedes the quench tower to separate the fuel oil fraction.
The cracked gas compressor is the plant's critical machine
The cracked gas compressor raises the entire product stream to the pressure the separation train requires, and it is the single largest rotating asset in the plant. There is no installed spare.
Coil outlet pressure is deliberately held as close to atmospheric as possible precisely to minimise pressure at the compressor suction, because compression duty drives both energy consumption and machine stress.
Between compression stages, condensed water and light gasoline are removed and the gas is washed with caustic or amine followed by caustic to remove carbon dioxide, hydrogen sulphide and Sulphur dioxide. The compressed gas is then dried with desiccant and cooled with propylene and ethylene refrigerants to cryogenic temperatures in the cold box for front-end demethanisation, depropanisation or deethanisation.
A cracked gas compressor failure stops the complex. Condition monitoring on that machine returns more than on any other asset on site.
Transfer line exchangers
Coke accumulates in the transfer line exchangers as well as the coils. After several coking and decoking cycles, typically every 3 to 4 months, the exchangers must be brought offline, cooled and cleaned mechanically, taking the whole furnace with them.
Conversion and Derivative Units
- Some petrochemical plants further process the recovered materials into downstream chemical products within the same complex.
- Ethylene converts into polyethylene or ethylene glycol. Propylene transforms into polypropylene or cumene. Aromatic compounds such as benzene and toluene produce styrene, phenol and other solvents.
- Companies integrate these derivative units within petrochemical complexes to minimize transportation and logistics costs. The operational consequence is tighter coupling: a derivative unit outage backs up into the olefins plant unless intermediate storage absorbs it.
Types of Petrochemical Plants

Petrochemical plants are classified into olefins, aromatics and syngas plants based on the products they produce. Olefins plants produce ethylene and propylene. Aromatics plants focus on benzene and toluene. Syngas plants produce chemicals such as ammonia and methanol.
Each type carries a different operational profile, a different critical machine and a different maintenance rhythm.
Olefins Plants
- These plants focus on producing ethylene and propylene, using steam crackers to convert ethane and propane from natural gas and naphtha from crude oil into these monomers.
- They are furnace-limited and compression-limited. Availability is governed by furnace run length, decoke duration and cracked gas compressor reliability, in that order.
- Olefins plants are also the most energy-intensive facilities in the sector, which makes utilities availability a production constraint rather than a support function.
Aromatics Plants
- Aromatics plants produce benzene, toluene and xylene from naphtha and other refinery streams, usually through catalytic reforming and extraction rather than steam cracking.
- The operational profile is distillation-heavy and catalyst-dependent. Availability is governed by column and heat exchanger fouling, catalyst life and the reformer regeneration cycle.
- Heat integration is extensive, which means a single exchanger cleaning can affect several columns.
Syngas Plants
- These use natural gas or coal to generate synthesis gas, a mixture of hydrogen and carbon monoxide, which then produces industrial chemicals such as ammonia and methanol.
- The reformer is the critical asset. Catalyst life, tube integrity and the reformer's own firing control set both output and turnaround timing.
- Syngas plants carry a distinct safety profile because of large hydrogen and carbon monoxide inventories, which drives relief system design and detection requirements.
Significance of Petrochemical Plants in the Oil and Gas Industry
Petrochemical operations are the highest value-add stage of the hydrocarbon chain, and they are also the stage where availability losses are most expensive per hour.
Because capital intensity is high and margins are driven by throughput, a petrochemical plant is evaluated on availability rather than on nameplate capacity. The commercial consequence of an unplanned outage is measured in days of lost production at full margin.
Value Addition to Crude Oil and Gas
- Converting hydrocarbons into chemicals captures substantially more value per unit of feedstock than burning them as fuel, which is why integrated refiners continue to invest in chemicals capacity.
- The operational implication is that chemical units are run hard and shut down reluctantly. That tension between throughput and maintenance is the central management problem in this sector.
Supporting Diverse Industries
Petrochemical output feeds automotive, textiles, electronics, healthcare and agriculture manufacturing, which means demand is tied to industrial production rather than to energy policy.
For a plant operator, the relevant consequence is contractual. Long-term offtake agreements with downstream manufacturers carry delivery obligations, and an unplanned outage becomes a supply failure rather than a production loss.
That is why reliability engineering in this sector is a commercial function and not only a maintenance one.
Enabling Innovation
- New materials development drives specification changes, and specification changes drive plant modification.
- A product grade change can require new catalyst, modified operating conditions or additional separation capacity, each of which is an engineering project with its own integrity and commissioning requirements.
- Plants that can execute modifications without extending turnaround duration hold a structural advantage over those that cannot.
Safety and Environmental Controls in Petrochemical Facilities

Petrochemical plants in the United States operate under OSHA Process Safety Management, 29 CFR 1910.119, which governs facilities handling threshold quantities of highly hazardous chemicals.
PSM has fourteen elements, including process safety information, process hazard analysis, mechanical integrity, management of change and incident investigation. Mechanical integrity is the element that connects directly to inspection practice.
Crucially, OSHA PSM and the EPA Risk Management Program cite API inspection standards as recognized and generally accepted good engineering practice, or RAGAGEP. That means API intervals are enforced indirectly through PSM audits rather than through direct citation of the API code.
A gap in a mechanical integrity programme becomes a PSM finding.
Insurance
Insurers assess process safety management, mechanical integrity records and turnaround discipline when pricing petrochemical risk. A documented programme with recorded findings and closed actions is underwriting evidence; an undocumented one is a question at renewal.
Advanced Monitoring Systems
Modern facilities rely on sensors and automated control systems to monitor temperature, pressure, and chemical composition in real time, with a distributed control system, or DCS, as the operational backbone.
A DCS executes regulatory control and presents the plant to the operator. A process historian stores time-series data at defined resolution, and it is the asset every analytics and performance application reads from.
Continuous data tracking keeps the process stable and within specification. It also provides the baseline against which a developing fault is detected, which is why historian resolution and retention are reliability parameters rather than IT settings.
When utilities fail
- The utilities system supplies steam, power, cooling water and instrument air to every unit on site. An interruption does not slow one unit; it trips the complex.
- Instrument air loss in particular drives control valves to their fail-safe positions across the whole plant simultaneously. Utilities reliability therefore carries a weight out of proportion to its capital cost, which is why many petrochemical sites run cogeneration.
Emergency Shutdown Systems
Emergency shutdown systems are safety instrumented systems that bring the process to a safe state automatically when defined conditions are exceeded, independently of the control system.
IEC 61511 governs functional safety for the process industry sector and defines safety integrity levels, or SIL, which express the required risk reduction for each safety instrumented function. SIL is determined by hazard analysis, not chosen by preference.
The independence requirement matters. A shutdown function sharing sensors, logic or final elements with the control system does not deliver the risk reduction the SIL assessment assumed.
Pressure relief systems provide the final mechanical protection layer, discharging to flare or to a containment system. Relief load calculation and flare system capacity are design parameters that must be revalidated whenever the process is modified, which is a management of change obligation under PSM.
Emission Controls
Petrochemical plants control emissions through flare systems, thermal oxidizers, scrubbers and selective catalytic reduction, each addressing a different stream.
A thermal oxidizer destroys volatile organic compounds by combustion, with regenerative thermal oxidizers recovering heat to reduce fuel use. Selective catalytic reduction, or SCR, converts nitrogen oxides to nitrogen and water across a catalyst using ammonia or urea. Scrubbers remove acid gases and particulates from vent streams.
Fugitive emissions are controlled through leak detection and repair, or LDAR, a structured programme of monitoring valves, flanges, pumps and connectors, documenting leaks and verifying repairs.
In the United States, National Emission Standards for Hazardous Air Pollutants under 40 CFR Part 63 apply to petrochemical process units, including specific subparts for synthetic organic chemical manufacturing.
Many facilities are also evaluating carbon capture to reduce carbon dioxide emissions, which carries a parasitic energy load that must be modelled rather than assumed away.
Permitting
Air permit conditions govern what the plant may emit and under what operating conditions. A modification that changes emissions potential triggers a permit review, and the permit timeline is frequently longer than the engineering timeline.
Wastewater Treatment
- Process water undergoes multi-stage treatment before discharge, typically combining oil and solids separation, biological treatment and polishing.
- Treatment removes contaminants generated during the manufacturing process and supports recovery of valuable materials, making the production process more resource-efficient.
- In the United States, discharge is governed by National Pollutant Discharge Elimination System permits under the Clean Water Act, with effluent limitation guidelines for organic chemicals, plastics and synthetic fibres manufacturing.
- Treatment plant upsets are a production constraint in their own right. A biological treatment system that loses its culture takes weeks to recover, and the plant cannot discharge in the meantime.
Petrochemical Plant vs. Petroleum Refinery
Though closely connected, these two facilities serve different purposes.
The codes and the process safety regime are shared. What differs is the equipment, the failure modes and the product slate.
Challenges Facing Petrochemical Industries

Feedstock Volatility
- The cost and availability of ethane, propane and naphtha fluctuate with crude and gas markets, and the spread between them determines which feedstock is economic to crack.
- Ethane crackers and naphtha crackers produce different product slates. An ethane cracker yields predominantly ethylene with limited co-products. A naphtha cracker yields a broader slate including propylene, butadiene and aromatics.
- That difference means feedstock economics are not simply a cost question. A shift in the ethane to naphtha spread changes which co-products are available to the market, which changes derivative unit economics downstream.
- Plants with feedstock flexibility can switch between them, at the cost of furnace retuning and a period of off-optimal operation.
Environmental Pressure
Scrutiny of the sector's carbon footprint is increasing, with pressure to reduce process emissions, control fugitive releases and adopt circular economy models including chemical recycling of plastic waste.
The operational consequence is that emissions control equipment is becoming a production constraint. A thermal oxidiser or SCR outage can limit which units may run, which makes emissions equipment part of the reliability programme rather than an environmental add-on.
Regulations tighten by amendment rather than by replacement, which means a compliance position established at commissioning drifts without anything changing on site.
Technological Complexity
Managing a petrochemical plant requires specialized equipment, experienced engineers and a structured mechanical integrity programme governed by API inspection codes.
API 570 sorts piping into classes by the consequence of a leak. Class 1, handling flammable or toxic fluids, requires external inspection at intervals not exceeding five years. Class 2 and 3 allow a maximum of ten years.
API 570 is the in-service counterpart to ASME B31.3, which is the design and construction code for process piping. API RP 580 provides the risk-based inspection methodology that can modify intervals across all three codes, with an authorized inspector approving any extension on documented analysis.
Turnarounds
- A turnaround is a planned total shutdown of a unit or complex for inspection, repair and replacement work that cannot be performed online. It is where most inspection findings are addressed and most major rotating equipment work is executed.
- Turnaround scope grows between planning and execution, and the discipline that controls cost is scope freeze rather than execution speed.
- The capital concentration is significant. The furnace section alone represents roughly 20 percent of the total cost of an ethylene plant, which is why furnace work dominates turnaround scope and schedule.
Staffing
The workforce constraint is specific rather than general. Furnace operations, rotating machinery and functional safety each require experience that takes years to build and is not easily contracted in.
Competition and Regulation
Global competition, trade policy and environmental regulation shape where new capacity is built and which existing capacity remains economic.
Regulatory regimes differ materially by jurisdiction. OSHA PSM, EPA RMP, 40 CFR Part 63 and NPDES are United States federal regulation. The European Union applies the Seveso III Directive, and the United Kingdom applies COMAH, each with its own major accident prevention requirements.
API and ASME standards are used internationally regardless of the regulatory regime, which means the engineering practice transfers even where the compliance framework does not.
The Future of Petrochemical Plants

Green Petrochemicals
- Bio-based feedstocks such as plant-derived ethanol can substitute for fossil-derived feed, and chemical recycling of plastic waste produces pyrolysis oil that can be cracked alongside conventional feedstock.
- Both change furnace behavior. Recycled and bio-based feeds carry contaminants that conventional feed does not, which affects coking rate, run length and separation train loading.
- The operational question is not whether the chemistry works. It is what the new feed does to furnace run length and to the integrity of equipment designed for a different feed composition.
Energy Efficiency Upgrades
- Energy efficiency in a cracker concentrates in two places: heat recovery from the cracking and distillation sections, and run length extension.
- Heat recovery systems capture thermal energy that would otherwise be rejected, reducing the fuel fired in the furnaces and the steam imported from utilities.
- Run length extension is an efficiency measure that is rarely classified as one. Anti-coking coil technologies roughly double run length, from about 30 days to up to 60 days, which removes decoke cycles, reduces thermal cycling on the furnace and recovers capacity.
Integration with Renewable Energy
- Some chemical plants are evaluating renewable electricity and, in a small number of cases, electrified cracking, though commercial deployment remains limited.
- The realistic near-term integration is in utilities rather than in the process. Renewable electricity supplied to a site reduces Scope 2 emissions from power consumption, and cogeneration producing both power and process steam remains the dominant configuration because the steam demand is continuous and large.
- Electrified steam cracking would displace fired furnaces entirely. It is in development and it is not yet an operating option at commercial scale.
Digital Transformation
Analytics, machine learning and predictive maintenance improve safety, maintenance planning and productivity, and all of them depend on the historian rather than on the algorithm.
A digital twin is a model of the plant running alongside it, fed by live data, producing an expected output against which real output is compared. The gap is the finding. It differs from a process simulation, which models design behavior with no live data.
Predictive maintenance on rotating equipment requires labelled failure history. Most plants record that a work order was raised and closed, not that a specific machine failed in a specific mode on a specific date, and that absence stops more projects than any modelling limitation.
Petrochemical Plants Fuel the Modern World
- Petrochemical plants convert ethane, propane and naphtha into the chemical building blocks that downstream manufacturing depends on, connecting refineries upstream to chemical producers downstream.
- What determines whether an individual plant performs is narrower than the chemistry suggests. Furnace run length of 20 to 60 days and a 1 to 3 day decoke cycle set the production rhythm. The cracked gas compressor sets the single-point risk. Utilities availability sets whether anything runs at all.
- Mechanical integrity under API 510, 570 and 653, enforced through OSHA PSM, sets whether the plant can legally continue operating between turnarounds.
- Those are the operational levers, and they are where reliability investment returns.
Partner with Prismecs for Reliable Petrochemical Plant Operations
Prismecs supports petrochemical facilities with engineering, equipment supply, installation and commissioning, operations and maintenance, and the supply chain behind them.
Delivered project scope includes eight TM2500 dual-fuel units totaling 260 MW at Birr, Switzerland, online in six months with a new 220 kV interconnection; four TM2500 units totaling 110 MW at Duqm, Oman, kept grid-ready with resident O&M crews, CMMS and parts support; an LM2500XPRESS plant at Miaoli, Taiwan delivered in ten months; and an LM6000 fleet decommissioned in Norway, transported and recommissioned at a new site.
That record is power generation, rotating equipment and electrical systems delivery. On a petrochemical site it applies to the utilities layer that every unit depends on, to cogeneration, and to the rotating equipment and controls that determine availability.
Capability spans petrochemical engineering services for the vertical, O&M services for the operating phase, I&C services for instrumentation, controls, SCADA and DCS support, EPC services for project delivery, owner's engineering for independent technical review, technology and consulting for assessment and options analysis, distributed energy solutions for site power and cogeneration integration, supply chain solutions for procurement, and equipment inventory for ready-to-ship rotating and electrical equipment.
One scope boundary worth stating. Prismecs supplies power, rotating equipment, electrical systems, controls and the supply chain supporting them. Process licensing, catalyst supply, furnace design and chemical process engineering are separate disciplines with separate providers.
Apply this article's criteria to any proposal, including ours. Ask which equipment the provider actually works on and under which codes. Ask what happens when an inspection finding lands mid-contract. Ask how they handle a turnaround scope increase. Ask who holds the records at handover.
To discuss utilities reliability, rotating equipment support, cogeneration or an operations and maintenance scope, send your facility type and configuration, connected and peak electrical load, critical machine inventory and turnaround cycle to sales@prismecs.com or call +1 (888) 774-7632.
Frequently Asked Questions About Petrochemical Plant
What is a petrochemical plant?
A highly engineered industrial facility that processes hydrocarbon feedstocks such as ethane, propane, naphtha and natural gas liquids into high-value chemical products including ethylene, propylene, benzene and their derivatives. These facilities operate through tightly controlled thermal, chemical and mechanical processes and are typically located adjacent to petroleum refineries to enable efficient feedstock transfer and shared utility infrastructure.
How does a petrochemical plant work?
Feedstock preparation separates and purifies raw hydrocarbons, followed by steam cracking at coil outlet temperatures of 750 to 850°C to break molecular bonds and produce ethylene and propylene. The cracked gas is quenched to 338 to 510°C, cooled in a water quench tower at 35 to 40°C, compressed, treated to remove acid gases, dried and cooled to cryogenic temperatures for separation, then passed to conversion units producing polyethylene, polypropylene and other derivatives.
What is furnace run length and why does it matter?
Run length is the period a cracking furnace operates before coke deposits force a shutdown for decoking. Steam cracking furnaces normally operate 20 to 60 days before a decoke is required. On a furnace-limited plant, where the cracker section caps overall output, run length directly determines annual capacity, which is why anti-coking coil technologies that roughly double it from 30 to 60 days are economically significant.
How long does decoking take and what does it cost?
A full decoke cycle typically takes 1 to 3 days and adds thermal cycling to the furnace. Feed flow stops, steam purges the coil, and a controlled steam and air mixture at 850 to 950°C oxidizes the coke until carbon dioxide concentration confirms the coil is clean. Every decoke removes production capacity, so on furnace-limited plants cutting hours per cycle recovers capacity almost as effectively as extending the run.
Why do identical furnaces have different run lengths?
Because the binding constraint differs. Two furnaces of the same design at the same plant can run cycles that differ by several hours, and the same furnace can run faster or slower between decokes. One may be limited by tube metal temperature, another by coil pressure drop, a third by transfer line exchanger fouling. That variability is why fixed calendar decoke schedules waste capacity.
What is the cracked gas compressor and why is it critical?
The machine that raises the entire cracked product stream to the pressure the separation train requires. It is the largest rotating asset in an olefins plant and there is no installed spare, so its failure stops the complex. Coil outlet pressure is deliberately held near atmospheric specifically to minimise pressure at the compressor suction, because compression duty drives both energy consumption and machine stress.
How often do transfer line exchangers need cleaning?
Coke accumulates in the transfer line exchangers as well as the radiant coils, and after several coking and decoking cycles, typically every 3 to 4 months, the exchangers must be brought offline, cooled and cleaned mechanically. That operation takes the whole furnace with it, which makes TLE fouling a scheduling constraint separate from the normal decoke cycle.
What is the difference between a refinery and a petrochemical plant?
A petroleum refinery converts crude oil into energy products like gasoline, diesel, jet fuel and LPG. A petrochemical plant takes hydrocarbon feedstocks, often supplied directly by refineries, and converts them into chemical building blocks. They share the same governing codes and the same process safety regime, and they differ in equipment, failure modes and product slate, with the petrochemical plant adding significantly higher value per unit of feedstock.
What are the three main types of petrochemicals?
Olefins, aromatics and synthesis gas derivatives. Olefins plants produce ethylene and propylene through steam cracking and are furnace-limited and compression-limited. Aromatics plants yield benzene, toluene and xylene from naphtha and refinery streams, with availability governed by exchanger fouling and catalyst life. Syngas plants convert natural gas or coal into hydrogen and carbon monoxide for ammonia and methanol, with the reformer as the critical asset.
Which safety regulations govern petrochemical plants?
In the United States, OSHA Process Safety Management under 29 CFR 1910.119 governs facilities handling threshold quantities of highly hazardous chemicals, with mechanical integrity as one of its fourteen elements. The EPA Risk Management Program applies alongside it. Both cite API inspection standards as recognized and generally accepted good engineering practice, which means API intervals are enforced through PSM audit rather than by direct citation.
What inspection intervals apply to petrochemical equipment?
API 510 sets 10 years internal and 5 years external for pressure vessels. API 570 sets 5 to 10 years by piping class, with Class 1 piping handling flammable or toxic fluids at not more than five years. API 653 sets 5 years external for atmospheric tanks with a 10-year internal baseline. API RP 580 provides the risk-based methodology that can modify all three, subject to authorized inspector approval on documented analysis.
What is IEC 61511 and how does it apply?
IEC 61511 governs functional safety for the process industry sector and defines safety integrity levels, or SIL, expressing the required risk reduction for each safety instrumented function. SIL is determined by hazard analysis rather than chosen. The independence requirement is critical: a shutdown function sharing sensors, logic or final elements with the basic control system does not deliver the risk reduction its SIL assessment assumed.
Why are utilities the single point of failure?
Because steam, power, cooling water and instrument air serve every unit on site. An interruption trips the complex rather than slowing one line, and instrument air loss drives control valves to their fail-safe positions across the whole plant simultaneously. Utilities reliability therefore carries a weight out of proportion to its capital cost, which is why many petrochemical sites run cogeneration producing both power and process steam.
How can a petrochemical plant improve energy efficiency?
Through heat recovery that captures and reuses thermal energy from cracking and distillation, reducing furnace firing and imported steam. Through run length extension, since anti-coking coil technologies roughly double run length from about 30 to up to 60 days, removing decoke cycles and recovering capacity. And through digital twins and predictive analytics that optimize equipment performance, which depend on historian data quality rather than on modelling sophistication.
Tags: Petrochemical Operations Steam Cracking Plant Reliability Mechanical Integrity Turnaround
recent posts
EPCM Services
19 minutes read
25 Questions to Ask a Power Plant EPC Contractor Before You Sign
Most lists of questions to ask an EPC contractor stop at the question. Get why each matters, the strong answer, the red-flag reply and a weighted bid...
Gas Turbines
19 minutes read
Dual-Fuel Gas Turbines: How Gas-and-Liquid Fuel Flexibility Works
A dual-fuel gas turbine switches from natural gas to diesel at load, but most failures start in idle oil lines. Get transfer steps and coking fixes be...
Power Utilities
18 minutes read
Temporary and Bridge Power for Industrial Facilities: When and How to Use It
Planning bridge power past 12 months? Under EPA rules your generators may be stationary from day one. Check Tier 4, NSPS KKKKa and SPCC triggers befor...
Gas Turbines
16 minutes read
What Is a Mobile Gas Turbine Power Plant? TM2500-Class Units Explained
A mobile gas turbine power plant is a transportable power generation system designed to add electrical capacity faster than a conventional permanent p...